 หัวกัดที่มีความแม่นยํา,เครื่องมือตัดสําหรับเครื่องจักรกลซีเอ็นซีทุกวัสดุ

When comparing a ball end mill vs flat end mill, start with the part feature rather than the tool price or coating. Choose a flat end mill when the drawing requires a flat bottom, สล็อต, ขั้นตอน, straight wall, or square shoulder. Choose a ball nose end mill when the surface is curved, blended, or three-dimensional.
If both feature types are present, use the flat end mill for stock removal and planar features. Then use the ball nose tool for curved-surface finishing. Tool price, การเคลือบ, and flute count should be considered only after the cutting-end geometry has been selected.
For available standard sizes and custom dimensions, ดูของเรา ดอกเอ็นมิลจมูกบอล.
คุณยังสามารถตรวจสอบของเรา flat end mills for slots, กระเป๋า, ไหล่, and other flat-bottom features.
การเปรียบเทียบอย่างรวดเร็ว: Ball End Mill vs Flat End Mill
| Decision Point | ดอกเอ็นมิลล์บอลโนส | ดอกเอ็นมิลล์แบบแบน |
|---|---|---|
| ปลายตัด | Fully rounded or hemispherical | Flat with defined outer corners |
| Choose It For | Curved, blended, and 3D surfaces | Flat-bottom and prismatic features |
| Typical Work | คอนทัวร์, การตกแต่งแม่พิมพ์, กึ่งสำเร็จ | การกัดหยาบ, ช่อง, การแทง, การกัดไหล่ |
| ผลลัพธ์พื้นผิว | More continuous on changing curves | Level on planar bottoms and faces |
| Internal Transition | Leaves a radius | Creates a sharp or near-square transition |
| Main Limitation | Inefficient on broad flat bottoms | May leave steps on complex curved surfaces |
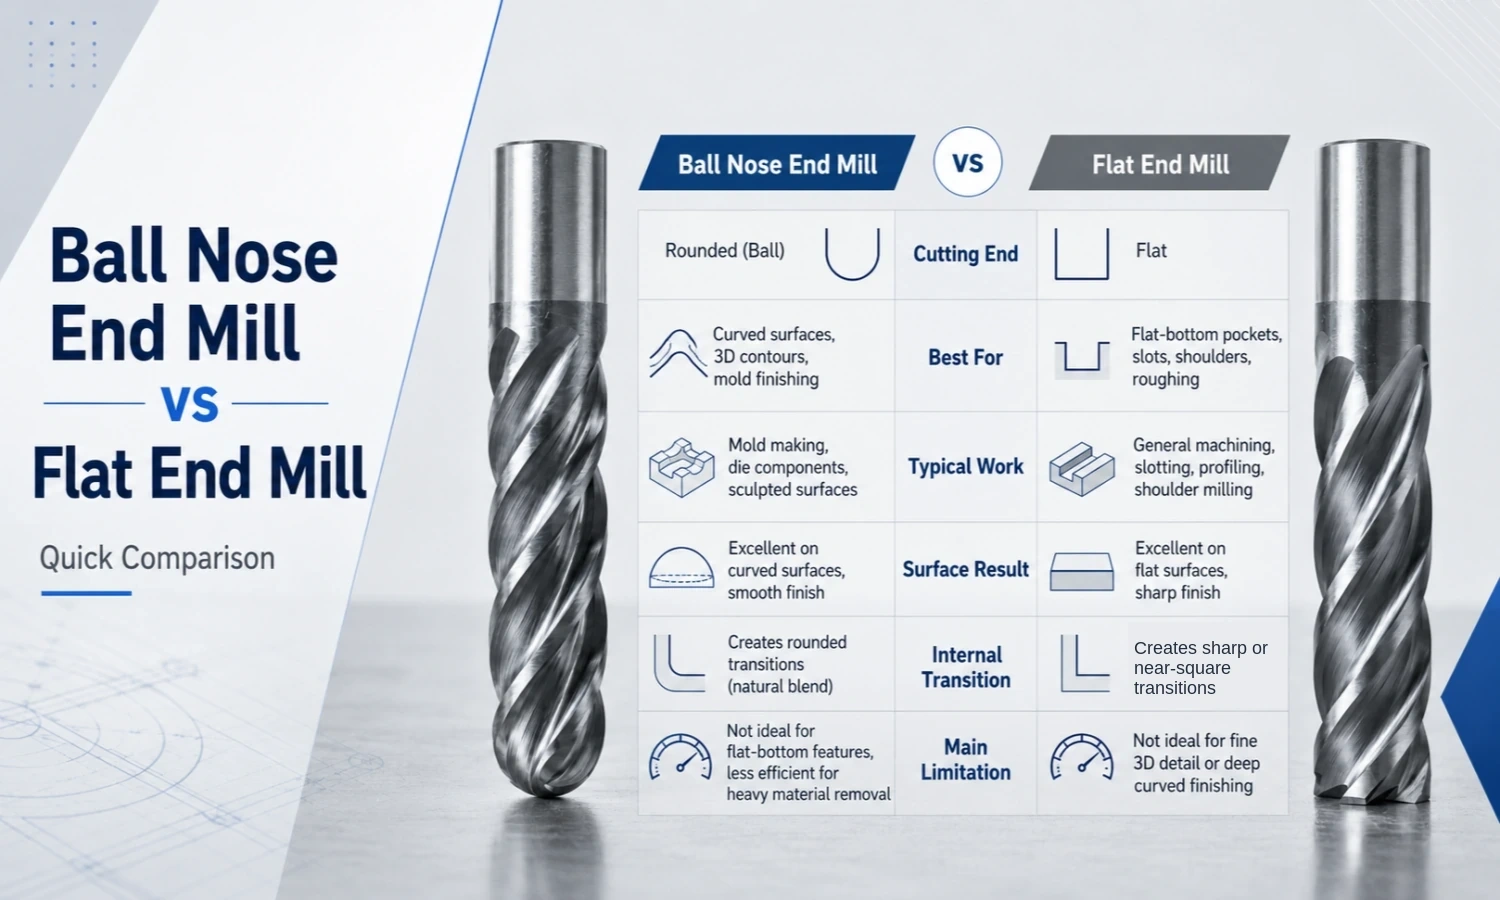
Read the table in this order: part geometry first, machining stage second, and required surface third. วัสดุ, ความเสถียรของเครื่องจักร, การเข้าถึงเครื่องมือ, การนับขลุ่ย, and coating are secondary checks.
What Is the Geometric Difference?
The main difference between a ball end mill and a flat end mill is not simply that one is round and the other is flat. Their cutting-end geometries create different contact conditions, which affect toolpath efficiency, การตกแต่งพื้นผิว, internal corners, and material removal.
เรขาคณิตของดอกเอ็นมิลล์บอลโนส
A ball nose end mill has a fully rounded cutting end. For a standard full-ball design, โดยปกติรัศมีปลายคมตัดจะอยู่ที่ครึ่งหนึ่งของเส้นผ่านศูนย์กลางการตัด. ตัวอย่างเช่น, ก 6 mm full ball nose commonly has an R3 profile.
อย่างไรก็ตาม, this relationship should not be applied to every radius cutter. Bull nose end mills and form tools use different cutting geometries.
The rounded cutting edge contacts only part of the workpiece at any moment. As the tool follows a slope or freeform surface, the contact point moves gradually around the ball.
ดังนั้น, the cutter can follow continuously changing surface angles without the abrupt contact changes that often occur with a flat cutting end. This is why ball nose tools are commonly selected for curved surfaces, blended profiles, โพรงแม่พิมพ์, และรูปทรงสามมิติ.
Flat End Mill Geometry
A flat end mill has a level cutting end and defined outer corners. The term square end mill is also widely used for this general cutting-end profile.
Because the end face can cut across a planar area, the tool can form flat bottoms, ผนังตรง, ขั้นตอน, and square shoulders efficiently. นอกจากนี้, the flat geometry creates a clearer transition between the bottom of a feature and its side wall.
The outer corner carries more cutting stress than a fully rounded tip. ดังนั้น, some flat end mills use a small edge preparation to improve corner strength. ยังไงก็ตาม, the tool remains a flat end mill rather than a bull nose cutter.
How Geometry Changes the Machining Result
Cutting geometry determines how the tool contacts the workpiece. That contact then affects scallop formation, staircase marks, toolpath spacing, การกำจัดวัสดุ, และคุณภาพพื้นผิวขั้นสุดท้าย.
Curved-Surface Contact, Step-Over, and Scallops
A ball nose end mill suits continuously changing surfaces because its rounded cutting edge can maintain contact as the surface angle changes.
Adjacent tool passes leave a small cusp, or scallop, on the machined surface. Reducing the step-over generally lowers the scallop height and improves the finish, but it also increases toolpath length and CNC cycle time.
The final result also depends on the ball radius, การหมดเครื่องมือ, ส่วนที่ยื่นออกมาของคัตเตอร์, ความแข็งแกร่งของเครื่องจักร, and toolpath direction. ดังนั้น, step-over should match the actual surface-finish requirement rather than simply being set as small as possible.
Flat-Bottom Contact and Square Shoulders
On a flat or prismatic feature, a flat end mill engages the bottom more directly. ดังนั้น, a level pocket floor or slot bottom can usually be produced with fewer passes.
The defined outer corner also creates a clearer wall-to-bottom transition. This makes a flat end mill suitable for:
- Flat-bottom pockets
- สล็อต
- ขั้นตอน
- ผนังตรง
- Square shoulders
- Planar surfaces
บนพื้นผิวโค้ง, อย่างไรก็ตาม, the flat cutting end approximates the shape through separate tool positions. If the step-over is too large, the toolpath may leave staircase marks.
A smaller step-over can reduce these marks. อย่างไรก็ตาม, the process becomes slower and may still require additional polishing or a ball nose finishing operation.
Material Removal and Machining Efficiency
สำหรับสล็อต, กระเป๋า, ขั้นตอน, and broad planar areas, a flat end mill normally removes material more efficiently.
More of its cutting end can engage the bottom of a flat feature. เพราะเหตุนี้, it can remove stock while also establishing the required flat surface.
โดยการเปรียบเทียบ, a ball nose end mill has a very low effective cutting speed near the center of its tip. When the center of the ball contacts a flat surface, it does not remove material as efficiently as the outer cutting area.
ดังนั้น, using a ball nose tool for heavy cutting across a broad flat bottom may create:
- Longer cycle times
- Lower stock-removal efficiency
- Additional heat near the tool center
- More tool passes
- Residual scallops
The opposite applies to complex 3D geometry. On a changing curved surface, the ball nose profile can maintain more consistent contact. ขณะเดียวกัน, a flat cutter may require much smaller steps and additional finishing passes.
When to Choose a Ball Nose End Mill
Choose a ball nose end mill when the workpiece contains continuously changing angles, พื้นผิวโค้ง, or complex three-dimensional geometry.
การใช้งานทั่วไปได้แก่:
– 3D contours and freeform surfaces
– Mold and die cavities
– Curved walls and blended radii
– Semi-finishing and final finishing of complex profiles
Its rounded cutting end follows changing surface angles more naturally than a flat end mill, helping reduce staircase marks and create a more continuous finish.
In mold machining, a flat end mill may remove most of the stock first, while a ball nose cutter is used for curved semi-finishing and final finishing.
สำหรับตัวอย่างการใช้งานเพิ่มเติม, อ่าน ดอกเอ็นมิลล์บอลโนสใช้ทำอะไร?
For available carbide cutters, ดูของเรา ดอกเอ็นมิลล์บอลโนส.
When to Choose a Flat End Mill
Choose a flat end mill when the drawing requires a flat bottom, สล็อต, ขั้นตอน, straight wall, square shoulder, or other planar feature.
การใช้งานทั่วไปได้แก่:
- Flat-bottom pockets
- สล็อต
- Steps and square shoulders
- Broad planar surfaces
A flat cutting end can establish the bottom and side wall more directly, making this geometry efficient for both feature machining and stock removal.
In parts that combine flat and curved features, the flat end mill often performs the initial roughing and planar machining before a ball nose tool finishes the curved areas.
For flat-bottom and prismatic machining, ดูของเรา Flat End Mills.
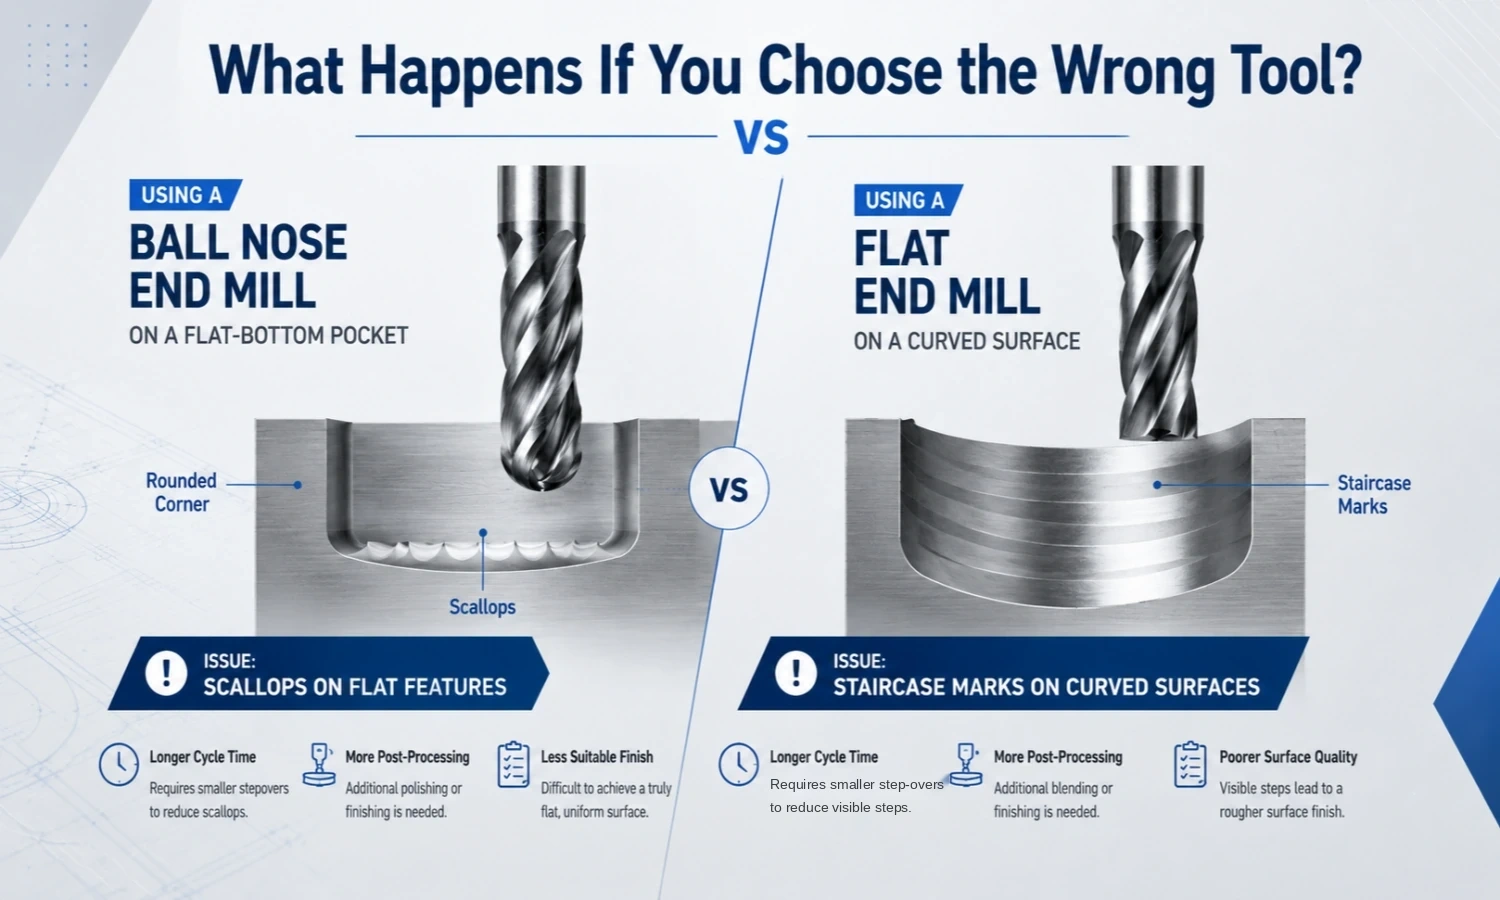
What Happens If You Choose the Wrong Tool?
Choosing the wrong cutting-end geometry can increase cycle time, leave unwanted tool marks, create extra polishing work, and produce a feature that does not match the drawing.
Using a Ball Nose End Mill on Flat Features
A ball nose cutter can remove material from a flat feature, but its rounded geometry does not form a flat bottom efficiently.
Using it for broad flat-bottom machining may result in:
- More tool passes and longer cycle time
- Residual scallops or an unwanted corner radius
- Additional polishing or rework
Cutting near the center of the ball is also less efficient than using the outer cutting area, so a flat end mill is normally the better choice for planar features.
Using a Flat End Mill on Curved Surfaces
A flat end mill can follow a 3D CNC toolpath, but its flat cutting face approximates a curve through a series of separate tool positions.
If the step-over is too large, visible staircase marks may remain. Reducing the step-over can improve the result, but it also increases toolpath length and machining time.
For demanding curved-surface finishing, a separate ball nose operation is usually more practical.
Can Ball Nose and Flat End Mills Be Used Together?
ใช่. In many CNC processes, using both cutters is more efficient than forcing one tool to complete every feature.
The flat end mill is selected where stock-removal efficiency and planar accuracy matter. The ball nose end mill is then selected where curved-surface continuity and finishing quality matter.
A Practical Roughing and Finishing Workflow
- Use a flat end mill to remove most of the stock and open pockets or slots.
- Finish flat bottoms, ผนังตรง, ขั้นตอน, and square shoulders with the flat cutter.
- Leave a controlled machining allowance on curved and blended areas.
- Use a ball nose end mill for semi-finishing to create a consistent surface.
- Apply the final ball nose toolpath with a step-over that matches the required finish.
This division of work is based on geometry rather than habit.
The flat tool handles operations where efficient stock removal and flat feature accuracy are required. The ball nose tool then handles surfaces where changing angles and finish continuity are more important.
วิธีการเลือก: A Practical Decision Process
The ball end mill vs flat end mill decision becomes easier when you start with the feature geometry:
- If the feature needs a flat bottom, สล็อต, ขั้นตอน, straight wall, or square shoulder, start with a flat end mill.
- If the feature is a 3D contour, curved wall, mold cavity, or freeform surface, start with a ball nose end mill.
- If the part contains both flat and curved features, use a flat end mill for stock removal and planar machining, then use a ball nose end mill for curved finishing.
After choosing the cutting-end geometry, consider secondary factors such as machining stage, surface-finish requirement, การเข้าถึงเครื่องมือ, ความแข็งแกร่งของเครื่องจักร, การนับขลุ่ย, และการเคลือบ.
For a detailed review of radius, เส้นผ่านศูนย์กลาง, เข้าถึง, การนับขลุ่ย, การเคลือบ, and material, ดู วิธีการเลือกดอกกัดปลายมน.
Common Mistakes to Avoid
Choosing by Diameter Instead of Feature Geometry
Two cutters with the same nominal diameter can behave very differently. Select the cutting-end geometry according to the workpiece feature before finalizing diameter, การนับขลุ่ย, or coating.
Ignoring Step-Over and Toolpath
Even the correct cutter can leave a poor finish if the toolpath is unsuitable. A large step-over may leave scallops with a ball nose tool, while a flat cutter may leave staircase marks on a curved surface.
การใช้ระยะยื่นของเครื่องมือมากเกินไป
Excessive tool overhang reduces rigidity and may increase vibration, การโก่งตัว, and visible tool marks. Use the shortest practical tool and overhang that can reach the feature.
ในที่สุด, do not judge the choice only by tool purchase price. A cutter that increases cycle time, polishing, rework, or scrap may create a higher total machining cost.
Ball End Mill vs Flat End Mill FAQ
Can a ball end mill make a flat-bottom pocket?
A ball nose cutter can remove material from the pocket, but it does not naturally form a complete flat bottom or sharp bottom corner. A flat end mill is normally the more efficient and accurate choice for this feature.
Can a flat end mill machine 3D surfaces?
ใช่, a flat end mill can follow a 3D toolpath. อย่างไรก็ตาม, the flat cutting end may leave staircase marks unless a very small step-over is used. For final curved-surface finishing, a ball nose cutter is usually more practical.
Which cutter is better for roughing?
A flat end mill is generally preferred for roughing flat, slotted, pocketed, or prismatic features because it removes stock efficiently while forming planar surfaces.
A ball nose tool may still be used for semi-roughing or semi-finishing inside complex curved cavities where a flat cutting end cannot follow the geometry effectively.
Still Deciding Which End Mill Fits Your Application?
เลือกก ดอกเอ็นมิลล์บอลโนส for curved, blended, and three-dimensional surfaces, หรือก ดอกเอ็นมิลล์แบบแบน for flat-bottom pockets, สล็อต, ขั้นตอน, และไหล่เหลี่ยม.
View Flat End Mills
If your part combines both flat and curved features, ส่งรูปวาดของคุณ, วัสดุชิ้นงาน, and machining requirements to sales@cutterbest.com, หรือติดต่อเราได้ที่ วอทส์แอพพ์ for tool-selection support.